10.2 Pressure, brazing and fire safety
A refrigerant circuit is a sealed pressure vessel. High-side pressure is typically 15–25 bar on R134a systems and 25–40 bar on R410A/R32 heat pumps and can exceed 100 bar on CO₂ systems. A loose flare or a cut pipe under pressure can whip, freeze skin or blow oil into eyes.
A pressure cooker is a good comparison. You never open the lid while it is whistling; you let pressure fall first. Treat every circuit the same way.
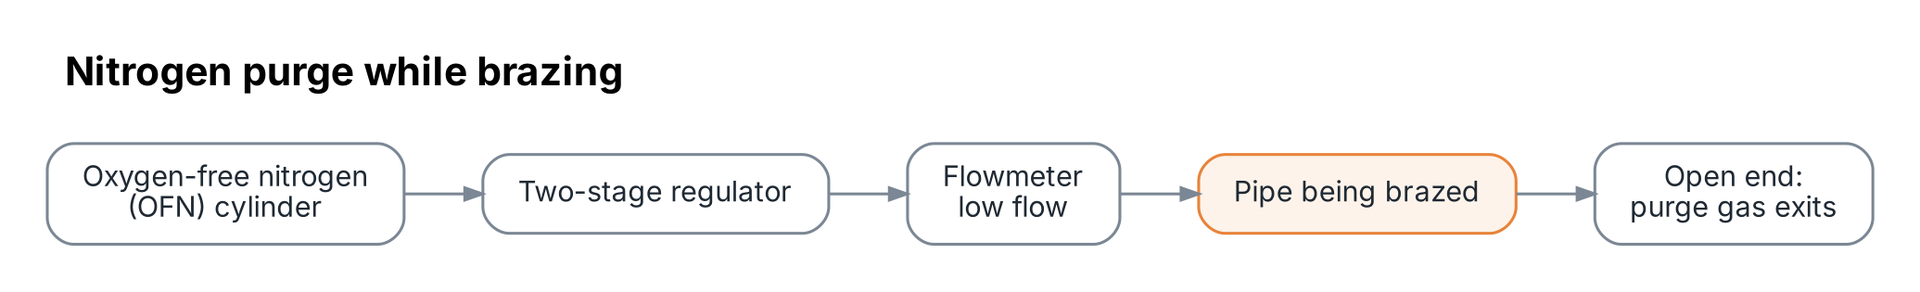
Brazing joins copper pipes with a filler rod at roughly 600–800 °C (typical). Blow dry nitrogen (oxygen-free nitrogen, OFN) through the pipe at low flow while brazing. This stops black copper oxide forming inside, which later blocks filters and expansion valves.
Never braze a circuit that still holds refrigerant or oil. Heat can raise pressure, and some refrigerants break down into toxic acids in a flame.
| Test | Purpose | Typical medium | Note |
|---|---|---|---|
| Strength / pressure test | Prove joints hold design pressure | Dry nitrogen | Use regulator and relief valve; never oxygen or compressed air |
| Leak test (standing) | Find leaks | Dry nitrogen, sometimes with trace gas | Hold for a set time, correct for temperature |
| Evacuation | Remove air and moisture | Vacuum pump | Typical target below 500 micron |
Worked example — pressure change with temperature during a standing test
A circuit is filled with nitrogen to 30 bar(g) at 25 °C in Chennai. Next morning it reads 29.2 bar(g) at 20 °C. Is it leaking?
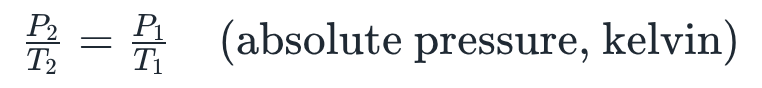
- P₁ = 30 + 1 = 31 bar(a); T₁ = 298 K; T₂ = 293 K.
- Expected P₂ = 31 × 293 / 298 = 30.48 bar(a) = 29.48 bar(g).
- Measured 29.2 bar(g) is 0.28 bar lower than expected — a small leak is likely. Re-check joints with soap solution.
Fire safety on site
- Hot-work permit where the site requires it.
- Keep a dry-powder or CO₂ extinguisher within reach.
- Remove or shield combustibles; use a heat mat.
- Stay 30 minutes after brazing to watch for smouldering (typical site rule).
Remember
- Recover refrigerant and depressurise before cutting or brazing.
- Always flow nitrogen while brazing; never use oxygen to pressure test.
- Use a regulator on every nitrogen cylinder.
- Correct standing-test readings for temperature.
Refrigerant circuits store energy as pressure, and brazing adds open flame — control both before you start.
There are no comments for now.
to be the first to leave a comment.